 1 / 4
Nano IR Heater
Nano IR Heaters represent cutting-edge infrared heating technology specifically engineered to achieve unprecedented thermal efficiency and precision heating performance in demanding industrial applications. These revolutionary heating systems combine advanced quartz infrared tubes with sophisticated diffusive reflective metal plates to concentrate radiant energy directly onto target processes, achieving extraordinary thermal efficiency levels of 95-99.8% while maintaining remarkably low external surface temperatures of just 40-80°C. This innovative design represents a paradigm shift in industrial heating technology, delivering superior performance while minimizing energy consumption and operational costs.
Ultra-high efficiency (95–99.8%)
Rapid heat-up in seconds
Low external surface temps (40–80°C)
- Ultra-compact, low-profile design for space-constrained installations
- Uniform, controllable infrared energy distribution with precision targeting
- Modular tube construction enabling easy maintenance and replacement
- Optional forced-air cooling for precise temperature control and extended life
- See all 14 features
Product Description
Key Features
- Ultra-compact, low-profile design for space-constrained installations
- Uniform, controllable infrared energy distribution with precision targeting
- Modular tube construction enabling easy maintenance and replacement
- Optional forced-air cooling for precise temperature control and extended life
- Corrosion-resistant stainless-steel housing for demanding environments
- Exceptional energy efficiency achieving 30-50% savings over conventional heating
- Instantaneous thermal response with zero warm-up time requirements
- Contamination-free operation suitable for cleanroom and sterile applications
- Advanced wavelength optimization for maximum material energy absorption
- Precise temperature control with integrated sensor and feedback options
- Extended service life exceeding 8 years with minimal maintenance requirements
- Custom configurations available for specialized heating applications
- Superior thermal uniformity eliminating hot spots and temperature variations
- Environmentally friendly operation with minimal energy consumption and emissions
Construction
- 01
High-Purity Quartz IR Tube
Advanced quartz tube construction housing precision heating elements for pure infrared output in the optimal 2-10 μm wavelength spectrum, ensuring maximum energy transfer efficiency.
- 02
Advanced Resistance Element
Premium FeCrAl or NiCr80/20 wire helically wound inside the quartz tube for uniform radiant emission, rapid thermal response, and extended operational life.
- 03
Precision Reflective Plate
Engineered diffuse reflective stainless-steel plate system to redirect and concentrate IR energy evenly across the target surface, maximizing heating efficiency and uniformity.
- 04
High-Performance Ceramic Insulation
1260°C-rated multi-layer ceramic fiber blanket insulation minimizing backside heat loss and maximizing forward radiation efficiency while providing thermal protection.
- 05
Precision Mounting Framework
Adjustable stainless-steel mounting brackets with custom positioning capabilities for secure installation, optimal heating alignment, and optional cooling system integration.
- 06
Optional Advanced Cooling System
Precision forced-air cooling module with temperature control to maintain optimal tube operating conditions, extend service life, and enable precise thermal management.
Specifications
- Heating Element Material
- FeCrAl Alloy, NiCr80/20 precision resistance wire
- IR Emission Spectrum
- Quartz tube, peak 2–10 μm wavelength output
- Reflective System
- Diffuse stainless-steel reflective plate assembly
- Thermal Insulation
- 1260°C ceramic fiber blanket multi-layer system
- Thermal Efficiency Rating
- 95-99.8% energy transfer efficiency
- External Surface Temperature
- 40–80°C during operation
- Service Life Expectancy
- >8 years (15,000+ hours) continuous operation
- Voltage Options
- Up to 480V AC/DC (custom configurations available)
- Power Rating Range
- 50W to 12 kW (custom ratings available)
- Response Time
- Instant heat-up in seconds
- Cooling System Integration
- Optional forced-air cooling modules available
- Housing Material
- Corrosion-resistant stainless-steel construction
- Environmental Rating
- Cleanroom compatible, contamination-free operation
- Control Integration
- PLC, automation, and precision control compatible
Applications
- Plastic extrusion and injection molding barrel preheating
- Web drying and curing in precision manufacturing lines
- Infrared heating tunnels and automated processing systems
- Precision preheating of dies, molds, and forming tools
- Coating and adhesive activation in manufacturing processes
- Laboratory and R&D high-efficiency infrared experiments
- Semiconductor wafer processing and electronics manufacturing
- Medical device sterilization and precision heating
- Food processing and pharmaceutical drying applications
- Automotive component heating and surface treatment
- Aerospace composite curing and material processing
- Precision welding and joining operations
- Surface activation and material modification processes
- Quality control and testing laboratory applications
Frequently Asked Questions
Available In
We manufacture the Nano IR Heater in India and export it to 20 countries. Choose yours for local supply details.
 Australia
 Russia
 Brazil
 Canada
 Germany
 Japan
 Kuwait
 Mexico
 Oman
 Qatar
 Saudi Arabia
 South Africa
 Turkey
 United Arab Emirates
 United Kingdom
 United States
 China
 Denmark
 India
 Thailand
Request a Quote for Nano IR Heater
Related Products
Component Heaters
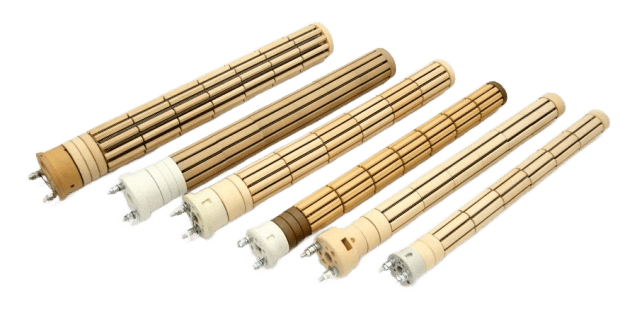
Bobbin & Pipe Heater
Bobbin & Pipe Heaters represent advanced industrial heating technology specifically engineered for efficient indirect heating of fluids, gases, and semi-solid materials in demanding industrial applications. These sophisticated heating elements utilize premium high-temperature refractory ceramic insulators available in various diameters and lengths, providing exceptional thermal stability and electrical insulation properties. The precision-engineered ceramic bobbin cores support high-quality NiCr or FeCrAl resistance wire coils, ensuring optimal heat transfer characteristics and long-term operational reliability in diverse industrial environments.
- Operate up to 800 °C
- Standard and custom bobbin diameters
- 100% immersion heat transfer efficiency
Component Heaters
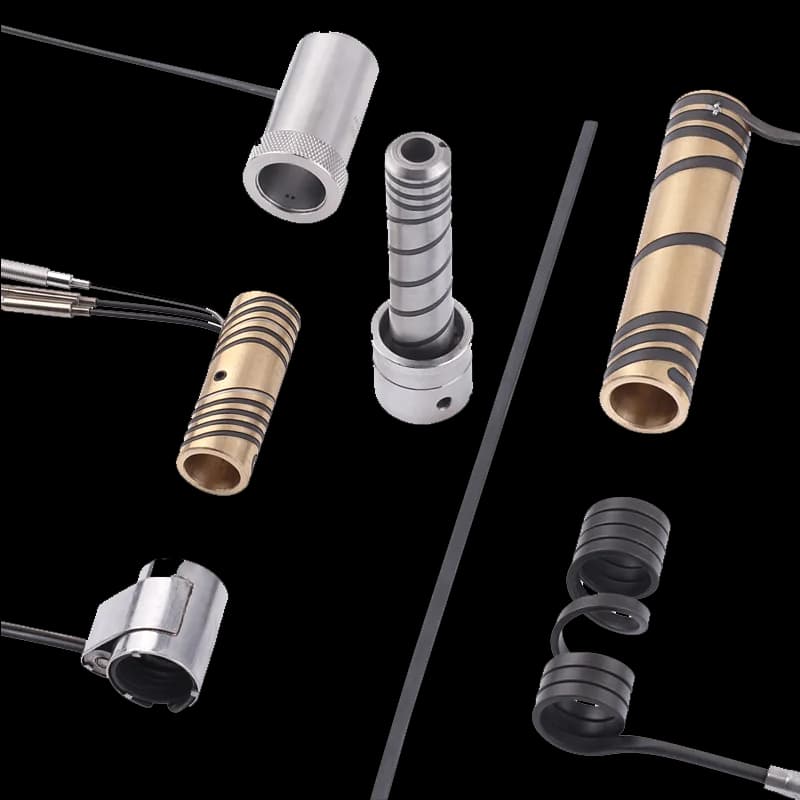
Coil & Hot Runner Heater
Coil & Hot Runner Heaters represent the pinnacle of precision-engineered heating technology specifically designed for high-performance plastic processing equipment and injection molding systems. These advanced heating elements are meticulously optimized for hot-runner injection molding systems, extrusion heads, dies, and specialized industrial applications requiring uniform, concentrated heat transfer with exceptional temperature control and reliability. The sophisticated engineering ensures optimal thermal performance in demanding production environments where precision heating is critical for product quality and operational efficiency.
- High-temp operation >250 °C
- Leak-proof fit around nozzle OD
- Rapid heat-up & tight temperature tolerance
Component Heaters
Silicone Rubber Heater
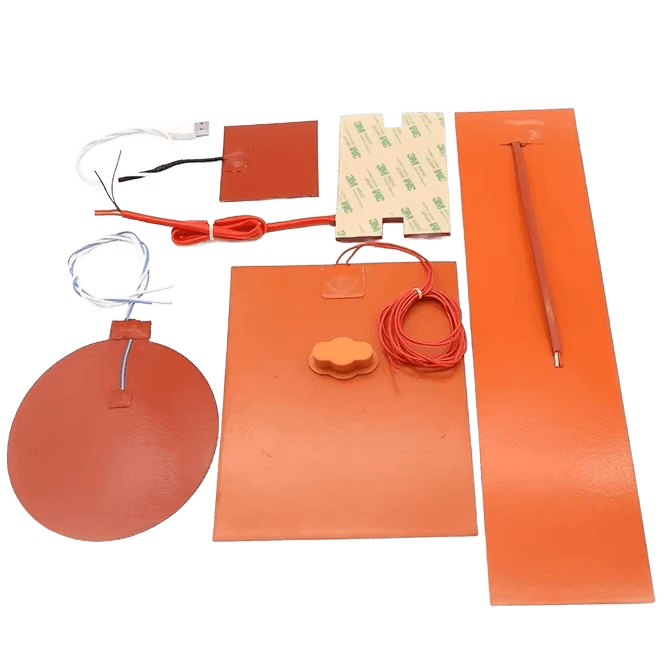
Silicone Rubber Heaters represent cutting-edge flexible heating technology engineered to provide uniform, reliable thermal solutions for complex geometries and demanding environmental conditions. These sophisticated heating elements are available in both wire-wound and etched-foil constructions, each optimized for specific application requirements and performance characteristics.
- Superior freeze protection capability down to –40°F
- Uniform heating performance up to 450°F continuous
- Exceptional flexibility and conformability to complex shapes
Component Heaters
Flameproof Drum Heater
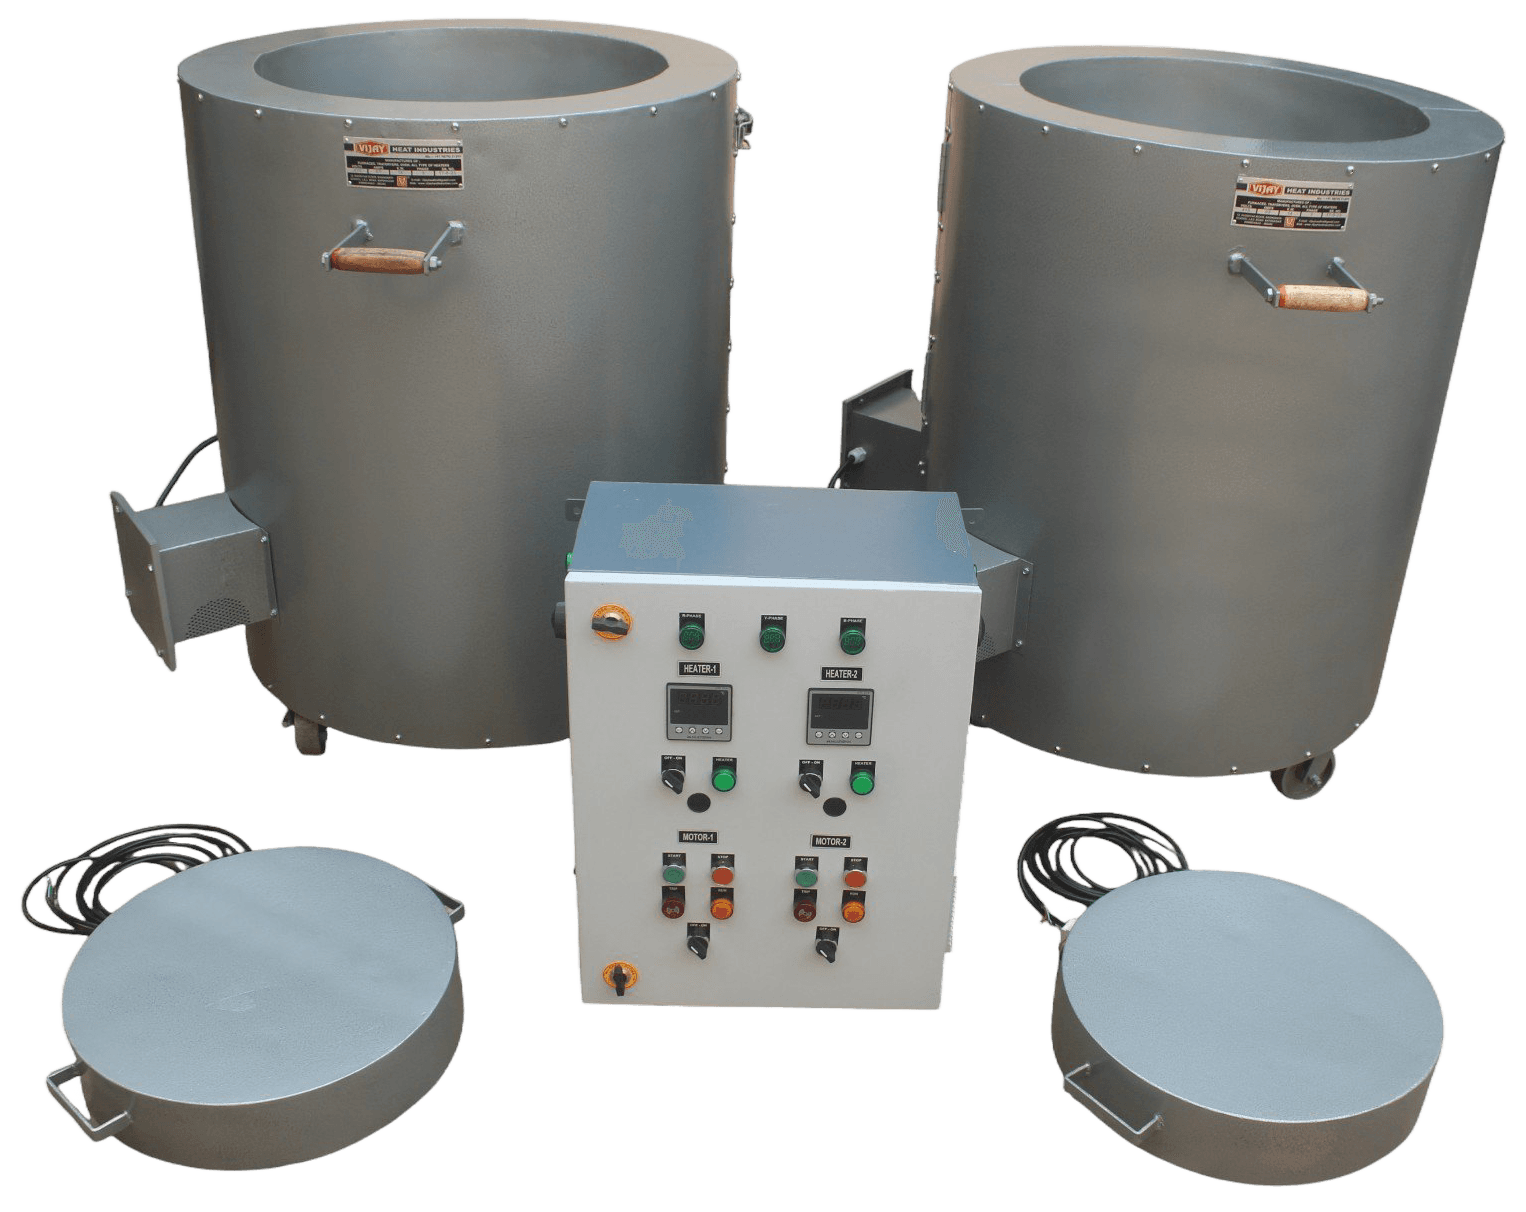
Flameproof Drum Heaters represent the pinnacle of safety-engineered heating technology specifically designed for hazardous industrial environments where explosive vapors, gases, or combustible dusts may be present. These advanced heating systems are meticulously engineered to meet the stringent requirements of ATEX (Atmosphères Explosibles) and IECEx (International Electrotechnical Commission Explosive) safety standards, ensuring completely safe operation in Zone 1 and Zone 2 classified areas without risk of ignition or explosion.
- Up to 200°C
- ATEX & IECEx Certified
- 0.5 kW to 4 kW
Interested in Nano IR Heater?
Get a custom quote from our engineering team.